

In the industry that is pressure sensitive, magic does not happen on the surface. The magic happens inside the sandwich. It’s not just about matching paper and film when you engineer a label. The key is to balance tension and moisture, as well as ensure that your die-cutting stations doesn’t cause a bottleneck on the converting line.
You risk tunneling, web breakage, or curling if you don’t consider the relationship between facestock and release carrier. The guide delves into the physics, chemistry and durability of laminates in order to optimize them for high-speed dispensing.
Defining Critical Face-Liner Combos
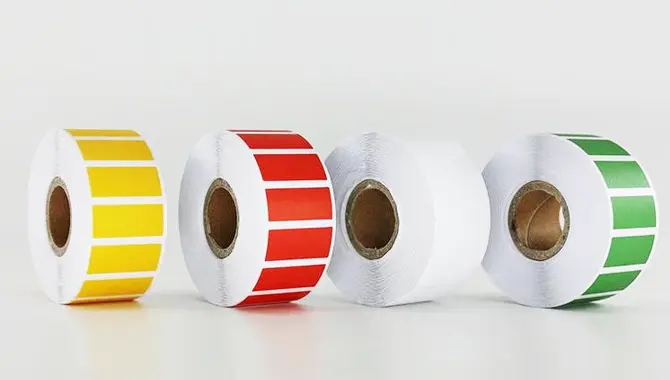
Face-liner combinations are engineered laminates of printable facestock and silicone-coated liner release, which is bonded with pressure sensitive adhesive. The composite structure is what determines the die-cutting speed, environmental stability and dispensing performance.
Physics of Dimensional Stability & Curl
Differential expansion is the main enemy of any laminated structure. You are effectively bonding materials that have vastly differing hygroexpansive characteristics when you combine a cellulosic face and a polymeric liner. Paper reacts to relative moisture (RH), whereas film responds mostly to thermal input.
You must maintain the right environment to ensure that your labels “layflat” or remain flat. Best practices in the industry suggest that storage and conversion environments be maintained at 23degC (+1degC), 50% RH (+-5%) and 2degC. The “forward curl” is caused when the liner does not move and the facestock absorbs water. In the opposite case, when the face contracts in dry conditions you will get “reverse cur.”
Field Insights: If your 80gsm semi gloss paper is being tunneled through a glassine 60gsm liner, you may want to consider using a poly-coated backside liner to equalize the moisture barrier. You can also use a combination of face and liner where both layers have similar hygroscopic properties.
Adhesive Rheology & The Sandwich Mechanics
Between your liner and face, the adhesive layer is acting as a viscoelastic coupling agents. It isn’t just about the stickiness, but also about the flow. It is important to evaluate both the Glass Transition (Tg), and the Rheology of the adhesive.
The cohesion between the waste matrix and the liner is crucial for high-speed stripping. You will notice “legging”, or adhesive strings, between the waste matrix liner and waste matrix if the cohesion of the adhesive is low. It is a common sign that your chosen face liner and adhesive are not matched.
Acrylic emulsions are typically available in a temperature range from -20degC up to +80degC. If your labeling application requires hot filling, then the SAFT (shear adhesion fail temperature) is the most important metric. It is important to have an adhesive that has a high level of shear resistance in order to avoid the label sliding onto the lining (flagging), before the product can be dispensed.
PET vs. Glassine: Liner selection
Your die cutting precision and speed will be determined by the release liner you choose. Here is a look at how the different technologies of liner impact on total construction.
| Feature | Super Calendered Glassine (SCK) | Polyester Film (PET) | Kraft Paper (CCK) |
|---|---|---|---|
| Caliper Consistency | Moderate (± 3-5 microns) | Excellent (± 1-2 microns) | Low (± 7-10 microns) |
| Tensile Strength | Medium | Very High | High |
| Die-Strike Sensitivity | Forgiving | Sensitive (Hard anvil required) | Very Forgiving |
| Sensor Transparency | Translucent (Optical sensors) | Transparent (Ultrasonic needed usually) | Opaque |
| Typical Application | Standard Prime Labels | Beer/Beverage (High Speed) | Sheeted Laser Labels |
Die-Cutting and Matrix Stripping Dynamics
The interaction between the cylinder of the anvil and the face-liner liner when you are converting specific combinations is crucial. This is called the “die strike.” You want to kiss the silicone without damaging the liners body.

The margin of error for a PET liner is very small (23-30 microns, e.g.). The liner can burst if a heavy die strike is used on PET. Glassine liners, on the other hand, compress. It is possible to cut the liner 3-5 microns deeper without damaging web integrity. Deep die-strikes can cause silicone to transfer onto the adhesive edge, which could kill the adhesion at the label’s edge. This is often misunderstood as “edge lifting.”
Common failure modes and their troubleshooting
Things can go wrong even with the best materials. How to identify failures using physical evidence
1. Pre-dispensing Separation (Tunneling)
It occurs when the face seperates from the liner and creates a tunnel. It is usually a problem with tension control during lamination, or an extreme humidity change. Rewind taper tension should be checked. To prevent inner cores from being crushed, you should use a hyperbolic or linear taper.
2. Poor Release (Tight release)
Your release force is too high if the label lifts up the liner at the beak of the dispenser. Release forces for high-speed standard dispensing should be between 10-30 grams/25mm. Check if your values are over 50g/25mm to see if it is because the adhesive wetted out too quickly over time or you chose a silicone-curing liner that has not been properly cured with a solvent adhesive.
3. The Ooze and Bleeding
Blocking is caused by adhesive ooze around the edges of the rolls. It is often caused by an excessive amount of winding tension, or the use of a high-flow “soft” glue on a core with a smaller diameter. Change to an adhesive that has a higher shear strength or lower your tolerance for coating weight.
FAQs
What are the best face-liner combos for a wet environment?
For wet environments, avoid paper-on-paper structures. Ideal is a Polypropylene or Polyethylene face with a PET liner. The combination of PP and PE is resistant to moisture. This prevents the label from lifting due to paper swelling.
What causes my die to wear out more quickly with some liners than others?
Magnetic dies are sanded with abrasive paper or liners that contain a high amount of clay (like some CCK grades). Film liners tend to be less abrasive but require more pressure in order to cleanly cut, and this can wear down the edge of your tool over many millions of rotations.
What face-liners can I apply with an ultrasonic scanner?
Clear-on-clear (Clear PET on PP) labels are perfect for ultrasonic sensors that detect differences in thickness (gap detection). Optical sensors work well for paper labels printed on glassine. They are also cheaper. Ultrasonic is “necessary” for most film-on films.
How does silicone transfer affect the performance of labels?
Silicone can be transferred to the adhesive surface if the anchorage of the silicone on the liner fails. The adhesive is “polluted” and the peel adhesion will be significantly reduced. You can detect this by looking at the loop tack value or by rubbing on the adhesive surface. It should be tacky and not slippery.
What is the effect of liner thickness on roll capacity?
The total laminate thickness is reduced by a significant amount when you switch from 60gsm (approx. 55 microns), to 30micron PET liners. You can fit up to 20-30% of labels onto the same-sized roll. This reduces the downtime during labelling line changeovers.

