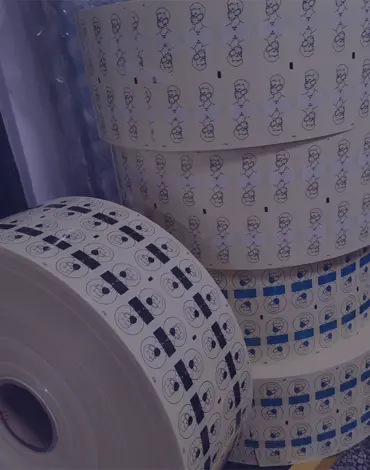
You’ve likely stood by a high-speed labeling applicator and wondered why some labels dispense like silk while others cause catastrophic web breaks. In my 15 years as a technical director in the self-adhesive industry, I’ve found that the answer almost always lies in the invisible architecture of the Silicone Coating. It is the silent enabler of the entire pressure-sensitive industry.
This guide deconstructs Silicone Coating technology from the perspective of material science and production efficiency. We will dive into the chemistry of polydimethylsiloxanes (PDMS), the physics of release force curves, and the mechanical precision required to maintain anchorage on diverse substrates like Glassine, PET, and CCK.
What is Silicone Coating in the Label Industry?
Silicone Coating is a thin, low-surface-energy functional layer applied to a release liner substrate to facilitate the controlled separation of a pressure-sensitive adhesive. This cross-linked polymer network provides the necessary release value for automatic dispensing while ensuring long-term chemical stability and preventing adhesive migration or silicone transfer.
In terms of label construction, the Silicone Coating serves as the critical interface between the carrier (liner) and the adhesive. Without high-quality anchorage of the silicone to the substrate, the entire laminate fails. The industry relies on specialized curing systems—thermal, UV, or electron beam—to transform liquid siloxanes into a durable, solid film that can withstand the rigors of die-cutting and environmental stress.
Chemistry and Curing: Thermal vs. UV Silicone Systems
Choosing the right Silicone Coating chemistry is a balance of substrate heat sensitivity and required release speed. In modern converting, we primarily categorize these systems based on their cross-linking mechanism. Each has a distinct Rheology and impact on the final Tensile strength of the liner.
| System Type | Curing Mechanism | Primary Benefit | Common Substrates | Cure Temp Range |
|---|---|---|---|---|
| Solvent-less Thermal | Platinum-catalyzed addition | Lowest stable release | Glassine, PET, Kraft | 120°C – 160°C |
| Solvent-based Thermal | Condensation/Addition | Superior anchorage | Specialty films, Foils | 100°C – 150°C |
| UV-Curable (Cationic) | UV Light / Photoinitiator | Heat-sensitive films | PE, PP, Thin PET | < 50°C |
| UV-Curable (Free Radical) | Acrylated Silicone | Instant curing speed | Digital print media | Ambient |
The Glass Transition Temperature (Tg) of the silicone network isn’t often discussed, but its impact on Cold flow is immense. If the silicone isn’t fully cross-linked, unreacted species can migrate into the adhesive, poisoning the Loop Tack and reducing the Peeling Adhesion (N/25mm). A professional setup targets a silicone extractable level of less than 5% to ensure performance integrity.
Release Force Curve and Automatic Dispensing Performance
The Release force curve is the DNA of your label’s performance. It defines how much force is required to peel the label at various speeds—from 10 meters per minute to over 300 meters per minute. A “flat” release profile is the holy grail for high-speed bottling lines.
To prevent pre-dispensing (labels flying off the roll) or web breaks, the Silicone Coating weight variance must be kept within ± 0.05 g/m2. If the coating is too thin, the adhesive may touch the liner substrate (pinholing), causing Adhesion spikes. If too thick, the cost increases without performance gain, and you risk Silicone transfer, which ruins the printability of the label face via back-side contamination.
Anchorage, Dyne Levels, and Substrate Interaction
Why does Silicone Coating stay on the liner? It’s all about Anchorage. For plastic liners like PET, the Dyne level of the film must be strictly monitored. A low dyne level leads to “rub-off,” where the silicone wipes away like dust under mechanical stress. We recommend a minimum surface energy of 38-40 dynes for filmic substrates before coating.
On paper liners like Glassine, the Opacity and smoothness of the paper affect the Silicone Coating weight tolerance. To prevent “strike-through” (silicone soaking into the paper fibers), a hold-out coating is often applied. This ensures the silicone stays on the surface where it belongs, maintaining a consistent Release value across the entire 10,000-linear-meter run.
Production Optimization: Tension and Die-Cutting
Applying Silicone Coating is a game of mechanical precision. The Tension profile of the web must be perfectly balanced. If the tension is too high during thermal curing, the liner will shrink upon cooling, leading to label curl. If too low, you get web weave and uneven coating distribution.
In the die-cutting stage, the silicone layer acts as a lubricant for the blade. However, the Anvil pressure must be set precisely to avoid Die-strike. If the die cuts through the Silicone Coating and into the liner, the adhesive will “key” into the liner fibers, making the label impossible to dispense. Specifically, aiming to reduce Physical Phenomenon such as liner bruising can extend the life of your rotary dies by 20%.
FMEA: Solving Common Silicone Failure Modes
When things go wrong on the press, you need an FMEA (Failure Mode and Effects Analysis) approach to troubleshooting. Most Silicone Coating issues stem from two factors: incomplete cure or substrate incompatibility.
- Issue: Silicone Rub-off. Cause: Low Anchorage or catalyst poisoning (often by sulfur or nitrogen compounds in the substrate). Solution: Check Dyne level and catalyst ratios.
- Issue: High Release Spikes. Cause: Silicone Coating weight variance or adhesive “interlocking” due to excessive Cold flow. Solution: Adjust the Rheology of the adhesive or increase coat weight.
- Issue: Adhesive Deadening. Cause: Silicone transfer. Solution: Verify cure using the “Heraeus test” and check extractables.
To prevent Shear Adhesion Failure (SAFT) at high temperatures, ensure the silicone is formulated for thermal stability. For automotive applications, Silicone Coating must remain functional within a range of -40°C to +150°C.
Technical Specifications for Quality Control
In our lab, we adhere to ISO and ASTM standards to ensure every batch of Silicone Coating meets the E-E-A-T (Expertise, Authoritativeness, Trustworthiness) criteria required for Tier-1 supply chains.
- Coat Weight (GSM): Typically 0.8 to 1.2 g/m2 for papers; 0.5 to 0.8 g/m2 for films.
- Extractables (%): Should always be < 5% for addition-cure systems.
- Release Value (cN/25mm): Standard release is 10-25 cN; Tight release is > 50 cN.
- Conformability: Must maintain integrity under 180° wrap angles during high-speed processing.
Frequently Asked Questions (FAQ)
1. How does humidity affect Silicone Coating?
While the silicone itself is hydrophobic, the substrate (like Glassine) is sensitive to moisture. Fluctuations in humidity can cause the liner to expand or contract, potentially cracking the Silicone Coating layer and causing Release value inconsistencies.
2. Can I use UV Silicone for all applications?
No. While UV Silicone Coating is excellent for heat-sensitive films, it generally has higher extractable levels than thermal systems. This makes it less suitable for medical or high-end pharmaceutical labels where migration is a concern.
3. What is the shelf life of a silicone-coated liner?
Under standard conditions (23°C, 50% RH), a Silicone Coating remains stable for 12 months. Beyond this, “release creep” may occur, where the Release force curve shifts upward due to adhesive aging.
4. How do I detect Silicone Transfer?
The easiest field test is the “marker test” or “tape test” on the back of the label face. If a permanent marker beads up or adhesive tape doesn’t stick to the back of the face material, you have Silicone transfer issues.
5. Is Silicone Coating environmentally friendly?
Silicones are inert and do not break down into microplastics. However, the challenge lies in recycling the liner. Modern processes are now available to strip the Silicone Coating, allowing the high-quality paper fibers or PET flakes to be reused in FSC certified streams.